Calculating air consumption means summing the flow rates of all connected devices weighted by their actual duty cycle, converting the result to a common reference state ANR or FAD, adding leaks and adding an operating margin. The resulting value is given in litres per minute or cubic metres per hour. It is recommended to verify it with a short-term flow measurement directly in operation, as manufacturers' catalogue data tends to be optimistic.
In brief:
- When calculating air consumption, it is necessary to convert the measured volumes to a uniform reference state and take into account leaks and an operating margin.
- The resulting flow rate is given in litres per minute or cubic metres per hour and should be verified by measurement directly in operation.
- To estimate the consumption of individual devices, a formula based on the number of strokes, volume per stroke and pressure is used, taking the duty factor into account.
- The total consumption is calculated as the sum of the flow rates of all devices with their duty cycles, to which leaks in the piping are added, which should be measured while the system is shut down.
- Continuous measurement and real-time monitoring help to more accurately detect leaks and adapt the sizing of the compressor station to actual operating conditions.
Contents
- Basic formulas and units for calculating air consumption
- Calculating air consumption for a pneumatic cylinder
- How to sum the consumption of all devices and account for leaks
- Measurement in practice: flow meters, sensors and continuous monitoring
- How to size a compressor based on the calculated consumption
- Step by step: from calculation to verification through measurement
- Experience with monitoring air consumption in practice
- How Kompresory-vzduchotechnika can help you with the calculation and sizing
- Frequently Asked Questions
Basic formulas and units for calculating air consumption
Before you start adding up the consumers, you need to master two things: converting volume to flow rate and understanding reference conditions. Without them, figures from different sources cannot be compared.
The volume a consumer uses per cycle is calculated as the piston (or diaphragm) area multiplied by the stroke. For a piston cylinder with a piston diameter of 40 mm and a stroke of 100 mm, the area is approximately 12.57 cm², so the volume per stroke is 125.7 cm³.
This volume is then converted to l/min by multiplying it by the number of cycles per minute. Ten cycles per minute at a volume of 125.7 cm³ gives approximately 1.26 l/min at operating pressure, but without correction for pressure.
This is where normalization comes into play:
- ANR (Atmosphère Normale de Référence) is a reference state according to the French standard, commonly used by European compressor manufacturers.
- FAD (Free Air Delivery) expresses the flow rate converted to the ambient air conditions at intake, i.e. the actual compressor output "drawn from the air".
- Both standards address the same problem: gas volume changes significantly with pressure and temperature, so without conversion to a common basis, consumption measured at 6 bar cannot be compared with consumption at 8 bar.
- The methodology for measurement and testing of compressors according to ISO 1217 defines how FAD is correctly determined under both laboratory and operational conditions, and it is the reference standard to which the rated values of most industrial compressors relate.
Calculating air consumption for a pneumatic cylinder
For an individual pneumatic cylinder, there is a simple formula established in technical practice:
Q = Z · (qp + qz) · n · 0.1
- Z is the number of cylinder strokes per minute (cycle frequency).
- qp is the volume of air required for the working stroke (in liters), qz is the volume for the return stroke.
- n represents the absolute pressure in bar (gauge pressure plus atmospheric pressure).
- The constant 0.1 converts the result into practical units of l/min.
Model example: a cylinder with a working stroke of qp = 0.05 l and a return stroke of qz = 0.04 l, a frequency of Z = 20 cycles/min, at a pressure of n = 7 bar absolute. Calculation: Q = 20 · (0.05 + 0.04) · 7 · 0.1 = 1.26 l/min. For hourly operation, this gives approximately 0.0756 m³/h.
There is a fundamental difference between single-acting cylinders, which consume air on only one stroke, and double-acting cylinders, where both directions of movement are counted. A double-acting cylinder therefore practically always has higher consumption at the same cycle frequency.
How to sum up the consumption of all devices and account for leaks
A single cylinder is easy to calculate. The problem arises when dozens of devices run simultaneously in a facility, each with a different duty cycle.
The basic formula for total consumption is as follows: Σ(qi · di) + Q_leak, where qi is the nominal flow rate of an individual device and di is the duty cycle factor expressed as the proportion of time the device actually draws air.
- A device running continuously has di = 1.0, while a pneumatic tool used only a few minutes per hour may have di around 0.1 to 0.2.
- For devices that never run simultaneously at full output, use a weighted average based on the actual operating cycle.
- For devices that may be switched on at the same time (typically several stations on one line), calculate the sum of their maximum consumption at the moment of overlap.
- Leakage (Q_leak) is included in the calculation as a separate item, because leaks in the distribution system consume air continuously, regardless of whether production is running.
Estimating leaks "on paper" tends to be inaccurate. A practice-proven approach is to measure consumption while production is shut down, when the only draw is from leaks.
Professional tip: If you don't have measuring equipment available, let the compressor run over the weekend, when production is shut down, and observe how often it cycles on. Every start means that air you've paid for is being lost through a leak into the system.
Measurement in practice: flow meters, sensors, and continuous monitoring
A calculation on paper is a starting point, not the final value. The actual consumption profile varies by shift, season, and the condition of the distribution system, which is why industrial practice combines calculation with measurement.
There are essentially three levels of technology available:
- Classic flow meters installed on the main branch or on individual sections of the distribution system, which provide an instant overview of consumption.
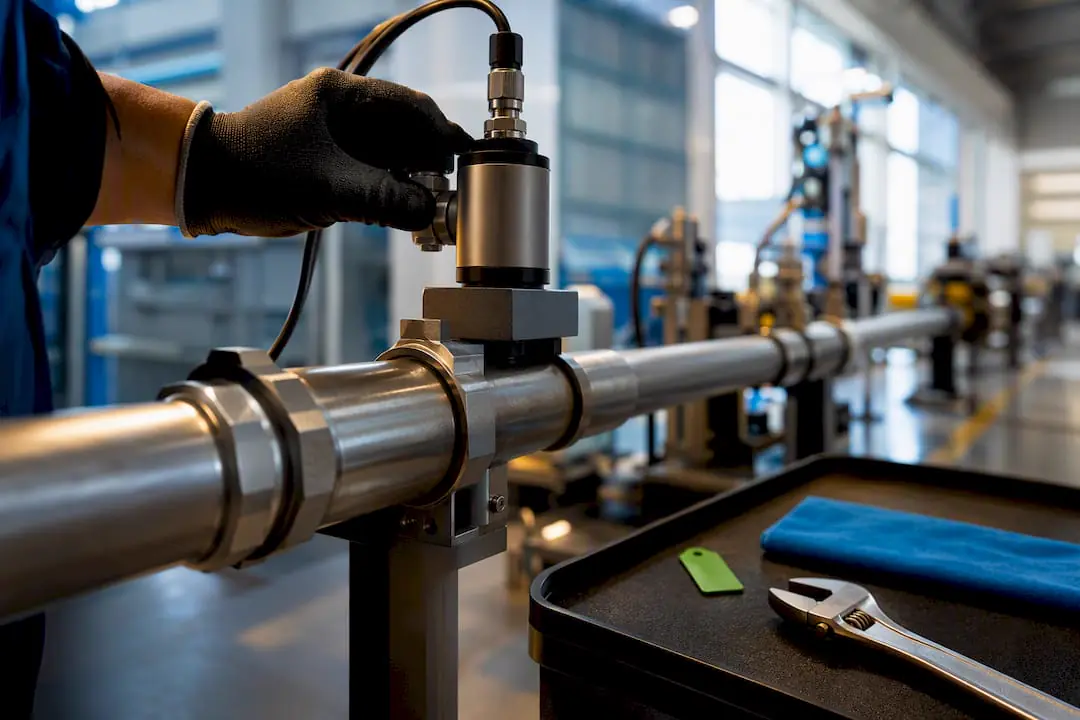
- Intelligent sensors with IO‑Link communication, for example the MP‑F series, which simultaneously measure flow, pressure, temperature and humidity and transmit data to the control system in real time.
- Cloud platforms for data collection, which generate graphs, reports and alarms from measured values when limits are exceeded, so you detect anomalies before they show up on your energy bill.
For a reliable consumption profile, it is recommended to measure at least one week of operation in order to capture all operating modes, including weekends and shift peaks. A shorter measurement can easily underestimate or overestimate actual consumption.
Continuous monitoring also allows early detection of a developing leak before it grows to tens of percent of total consumption, and gives the operations engineer utilization statistics from which to plan a potential expansion of the compressor station.

How to size a compressor according to calculated consumption
The calculated and measured consumption value is an input, not the final figure for selecting a compressor. Between the calculation and the purchase, there is still a decision regarding reserve and control.
- The target compressor flow is determined as the average consumption increased by a reserve for peak demand and possible future production growth, usually tens of percent above the average.
- The size of the air tank (reservoir) dampens short consumption peaks and reduces the number of compressor switching cycles, which extends its service life.
- For operations with variable demand, it is worth considering speed control or a combination of a smaller and a larger compressor, so the machine does not run unnecessarily at full power during low demand.
An overview of the compressor product range helps compare performance classes according to the calculated flow and choose the reserve level appropriate for your operation.
Step by step: from calculation to verification by measurement
It makes sense to divide the entire procedure into five steps that follow one another and can be repeated in any operation.
- Data collection – list the technical data sheets of all consumers, their rated flow rate and the actual number of cycles per shift.
- Calculation of Σ(qi · di) – for each consumer, determine the duty factor and multiply it by the rated flow rate.
- Adding leaks and a safety margin – add the estimated or measured leakage to the total and increase the value by a safety margin.
- Deploying measurement – install a flow meter or sensor and compare the measured profile with the calculation over at least one week of operation.
- Adjusting the sizing – based on the difference between the calculation and the measurement, adjust the compressor size, or alternatively identify leaks for repair.
Professional tip: Start with a rough estimate based on rated values, but never end the sizing there. A short measurement on the key branches of the distribution system will reveal differences that catalog figures will never capture.
Experience with monitoring air consumption in practice
From the dozens of operational audits we encounter at Kompresory-vzduchotechnika, one recurring issue stands out: companies calculate consumption based on nameplate values and then wonder why the compressor runs three times longer than it should. Diagnosing and eliminating leaks can bring significant energy savings, as can implementing continuous consumption measurement thanks to better control of the compressor station. I recommend a professional audit wherever the operation lacks its own measuring equipment, or where the results of DIY measurement differ substantially from the calculation.
— Zdeněk
How Kompresory-vzduchotechnika can help you with calculation and sizing
A calculation on paper is a good first step, but only a combination of measurement and professional assessment of the distribution system's condition provides real certainty. We offer a combination of measurement, component supply and service all in one place, so the customer doesn't have to deal with these services from multiple suppliers.
We provide consumption measurement directly on site, the design of a suitable compressor size based on the measured data, the supply of compressed air treatment units up to 18 bar and filtration according to the compressed air filtration program per ISO 8573, as well as installation and subsequent service. If your current calculations do not match the actual consumption, or if you suspect significant leaks, contact us with an inquiry for measurement or an energy audit. We will be happy to design a solution tailored to your specific operating profile.
Frequently Asked Questions
How to calculate air consumption for an entire facility?
Sum the nominal flow rates of all consumers weighted by their duty factor, add the measured leakage and a safety margin, then convert the result to a common reference condition ANR or FAD.
How to calculate air consumption from the compressor's power input?
Motor power input does not directly determine air flow, as it depends on efficiency and pressure. The actual flow (FAD) can be found on the compressor's nameplate or verified by measurement with a flow meter under the given operating conditions.
How to determine air consumption if I don't have technical data sheets?
The fastest way is short-term measurement using a portable flow meter or an IO‑Link sensor directly on the main branch of the distribution system, ideally for a period of at least one week of operation.
What is the difference between ANR and FAD when calculating air consumption?
ANR is a reference condition defining standard pressure, temperature, and humidity conditions, while FAD expresses the actual compressor output converted to these intake conditions. Without this conversion, flow rates measured at different pressures cannot be compared.