
TL;DR:
- The safety valve is a key active protection in compressor systems.
- The correct setting and dimensioning of the valve are fundamental for safe operation.
- Certification and a precise calculation of the capacity of the valve minimise the risk of failure and danger.
In practice the safety valve is often understood as a passive backup which is activated only in exceptional situations. That is a fundamental error. A badly designed or incorrectly set valve can cause the destruction of the air receiver, damage to the piping or a direct danger to the operator. Every technician working with compressors or pneumatic systems must understand not only what a safety valve does, but also how to dimension, set and maintain it correctly. This article brings a technical overview of the function, the calculation of the capacity and the most frequent problems you encounter in industrial practice.
Contents
- What a safety valve is and why it is essential in compressor systems
- The principle of operation and setting of the opening and closing pressure of the valve
- How to calculate the capacity of a safety valve correctly for various types of media
- The most frequent problems and modern trends in the use of safety valves
- What most technicians do not pay attention to when choosing safety valves
- A solution and an offer of professional components for the safety of air technology
- Frequently asked questions
Key findings
| Point | Details |
|---|---|
| Function of the safety valve | The safety valve protects the system from excessive pressure and must be set and checked correctly. |
| Pressure setting according to the standard | The opening and closing pressures must correspond to the requirements of the system and the valid standards for safety. |
| Correct calculation of the capacity | The choice of the capacity of the valve proceeds from the maximum possible overpressure and the procedure laid down by the API, ASME or ČSN standards. |
| Solving operating difficulties | Modern trends place the emphasis on certification, new materials and the regular maintenance of the valves. |
What a safety valve is and why it is essential in compressor systems
A safety valve is a mechanical device which automatically opens the flow cross-section when the set pressure in the system is exceeded. As soon as the pressure falls to the closing value, the valve closes again. It works without an external power supply, without control electronics. Mechanical reliability is its main advantage.
In compressor systems the safety valve fulfils the function of active protection, not of a mere backup. The air receiver, the pipe distribution lines and the connected equipment have a defined maximum working pressure. In the event of a failure of the pressure switch or a failure of the regulation, the pressure can rise uncontrollably. Without a functioning safety valve a mechanical failure of the pressure vessel is a risk, which can have fatal consequences.
The key properties of a reliable safety valve:
- Certification according to the valid standards (ČSN EN 1488, PED 2014/68/EU)
- A precisely set opening pressure corresponding to the maximum working pressure of the system
- Sufficient flow capacity for leading away the medium at the full output of the compressor
- Resistance of the materials to the medium (air, nitrogen, aggressive gases)
- Mechanical resistance to vibrations and temperature fluctuations
For industrial operation it holds that safety valves for compressors must meet strict requirements on the repeatability of the function. A valve which has opened once and then does not seal is just as dangerous as a valve which does not react at all.
“The safety valve is the front line of protection of the system, it must be mechanically reliable and certified." This principle applies without exception to every industrial compressor system.
Certification is not a formality. A valve without valid certification cannot legally be operated in pressure equipment subject to the PED directive. The inspection technician always verifies the state and certification of the safety valve too when checking a pressure vessel. A poor-quality or uncertified valve means a direct risk for the operator as well as for the insurance cover of the plant.
The principle of operation and setting of the opening and closing pressure of the valve
After establishing why the valve is key, let us look at its precise mechanical action.
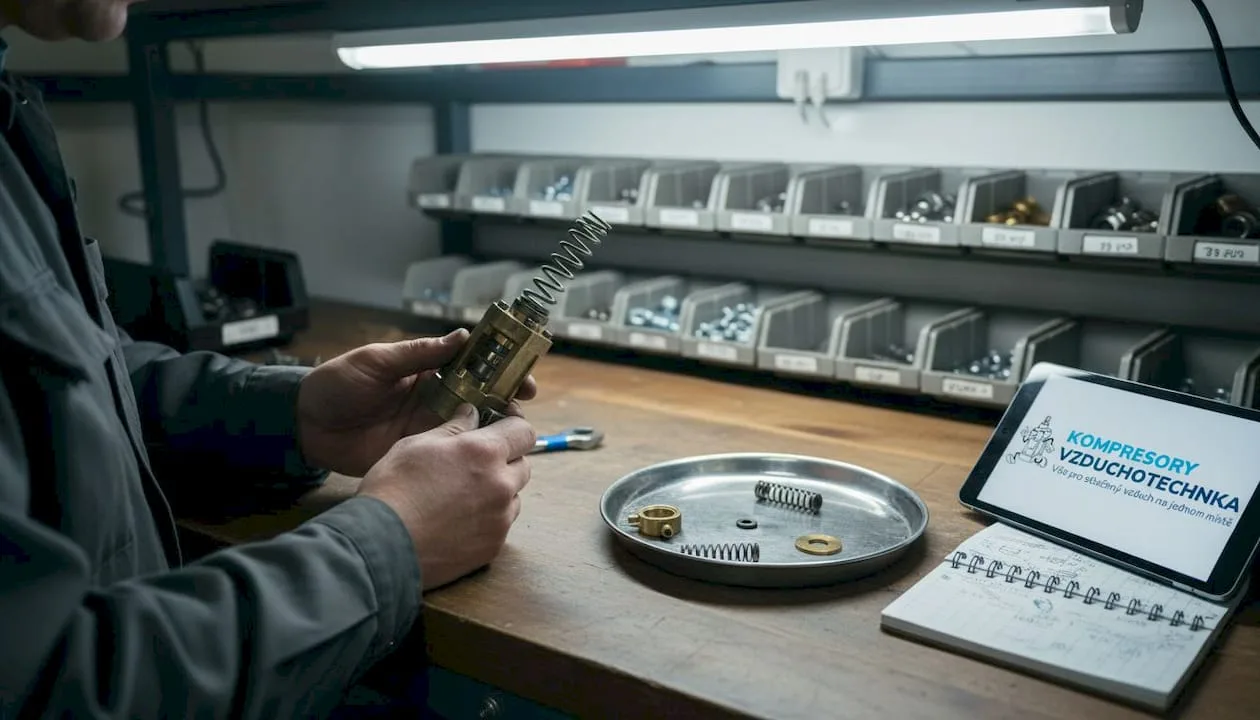
The safety valve works on the principle of overpressure balancing. A spring holds the closing element (a ball or a disc) in the seat. As soon as the force from the pressure of the medium overcomes the preload of the spring, the valve opens and begins to lead away the medium. The opening pressure is the value at which this phenomenon occurs.
The closing pressure is always lower than the opening one. The closing overpressure is 0.8 times the opening pressure. That means that a valve set to open at 10 bar closes at approximately 8 bar. This difference is intentional and prevents rapid oscillation of the valve (so-called chattering).
| Parameter | Typical value | Note |
|---|---|---|
| Opening pressure | According to the setting (e.g. 10 bar) | Must correspond to the max. working pressure |
| Closing pressure | approx. 80 % of the opening one | Defined by the standard |
| Tolerance of the setting | ±3 % | According to ČSN EN 1488 |
| Back pressure (backpressure) | Max. 10 % of the opening one | Influence of the discharge piping |
A problem arises when the supply pressure of the system exceeds the closing pressure of the valve. In such a case the valve stays slightly open and begins to seep. That is not a defect of the valve, but a mistake in the dimensioning of the system. The solution is the insertion of a reducing valve before the safety valve, or resetting the pressure switch of the compressor.
Precise settings are important also from the point of view of the most frequent mistakes in using a compressor. Many operators set the safety valve unnecessarily high so that the valve does not “open unnecessarily". In doing so, however, they reduce the safety margin of the system.
Professional tip: If the safety valve repeatedly seeps after opening, first check the supply pressure. If the supply pressure is higher than the closing pressure of the valve, the valve cannot close correctly. This is the most frequent cause of a repair of an air leak in compressor stations.
The correct setting of the opening pressure must respect the maximum allowable pressure of the pressure vessel (MAWP). The safety valve must not be set higher than the MAWP value. Conversely, too low a setting causes unnecessary opening in normal operation and accelerates the wear of the seat of the valve.
How to calculate the capacity of a safety valve correctly for various types of media
With an understanding of the mechanics of the valve one must also master its correct dimensioning according to the operating needs.

The capacity of the safety valve states what quantity of the medium the valve can lead away when fully open. It is not enough for the valve merely to open. It must be able to lead away a sufficient quantity of the medium so that the pressure in the system does not fall more slowly than it rises. An underestimated capacity of the valve is just as dangerous as no valve.
The procedure for calculating the capacity:
- Determine the maximum flow of the medium generated by the source (output of the compressor in m³/min or l/min)
- Establish the maximum allowable overpressure of the system (MAWP in bar or kPa)
- Choose the overpressure tolerance according to the standard (+10 % for one-off events, +21 % for fire situations according to API 520)
- Recalculate the capacity for the specific medium (air, nitrogen, steam) with a correction for density
- Verify the result against the catalogue values of the manufacturer of the valve
For air and gases different calculation formulas apply than for liquids. With gases the compressibility of the medium plays a role, with liquids the calculation is simpler. The choice of the capacity must correspond to the maximum overpressure of the system, the recalculation according to API 520 and ASME for +10 to 15 %.
| Type of medium | Standard of calculation | Overpressure tolerance | Correction factor |
|---|---|---|---|
| Air and gases | API 520, ASME VIII | +10 % (operation) | According to the density of the gas |
| Liquids | API 520 Part I | +10 % | 1.0 (water as a reference) |
| Steam | ASME I, EN 13445 | +3 % (boilers) | According to the enthalpy |
| Fire situation | API 521 | +21 % | A specific calculation |
A practical example: A compressor with an output of 500 l/min and a working pressure of 8 bar. The maximum overpressure of the system is 10 bar. The safety valve must be able to lead away at least 500 l/min at a pressure of 10 bar. When choosing from the catalogue you choose a valve with a capacity of at least 10 % above this value as a safety margin.
It is also important to respect the safety rules for work with a compressor and the valid standards for safety valves, which define the minimum requirements for the flow cross-section and the test conditions. Underestimating the capacity is in practice a much more frequent mistake than overestimating it.
The most frequent problems and modern trends in the use of safety valves
After mastering the calculation of the capacity it is useful to know the practical pitfalls and novelties of the field too.
The most frequent operating problems with safety valves can be divided into several categories:
- Leakage after opening: Caused by deposits of impurities in the seat of the valve or damage to the sealing surface. Solution: cleaning or replacement of the valve.
- The valve does not open on reaching the set pressure: Corrosion or mechanical seizing of the spring. A critically dangerous state requiring immediate replacement.
- Chattering (oscillation of the valve): The valve opens and closes rapidly. Cause: too small a difference between the working and opening pressure, or an underestimated capacity of the valve.
- Premature opening: Wear of the spring or an incorrect setting. It causes unnecessary losses of the medium and accelerates the degradation of the seat.
- Corrosion and contamination: Especially in applications with damp air or aggressive media.
Empirical data on the function of safety valves are missing in open sources. The standards place the emphasis on empirical formulas and tolerances, not on statistical data from operation. That means that the technician has to proceed from the normative requirements and their own operating experience.
Modern trends in the construction of safety valves include the use of stainless steel and special polymers for the sealing elements, which extend the service life in aggressive environments. Certification according to SIL (Safety Integrity Level) is becoming the standard in the process industry. Valves with the possibility of manual release (so-called test lift) make regular functional tests possible without the need for dismantling.
Professional tip: Carry out a functional test of the safety valve at least once a year. For valves on air receivers with operation over 200 hours a year we recommend a test every 6 months. A short manual release of the valve is enough to verify that the moving parts have not seized. More about the principles of safe pneumatics can be found in the article about decompressors in pneumatics.
A regular inspection includes a visual check of corrosion, verification of the pressure setting and a test of the function. Valves with damaged paint or visible corrosion on the body must be replaced regardless of their apparent functionality. Corrosion on the surface signals a possible degradation of the internal components.
What most technicians do not pay attention to when choosing safety valves
From a practical point of view it is important to uncover the details which ordinary instructions often omit.
Most technicians choose a safety valve according to two parameters: the opening pressure and the threaded connection. That is not enough. An overlooked factor is the back pressure (backpressure) on the discharge side of the valve. If the outlet of the valve is connected to a common pipe or into an enclosed space, the back pressure reduces the effective opening pressure of the valve. The valve then opens earlier than it was set.
Another underestimated aspect is the dynamic behaviour of the system. With a rapid rise in pressure (for example in the event of a failure of the regulation of a rotary screw compressor) the pressure can exceed the set value before the valve manages to open fully. Valves with a slow response are unsuitable in such applications.
Certification of the valve is not only an administrative requirement. A certified valve has a verified repeatability of function, defined tolerances and documented test conditions. An uncertified valve can work correctly on the first opening and fail on the second. The specifics of safety valves in various designs must be known before choosing for a specific application. The investment in a certified valve is always lower than the cost of repairing the damage caused by its failure.
A solution and an offer of professional components for the safety of air technology
If you are looking for a proven technical solution corresponding to the latest standards and requirements, we recommend a qualified offer of components.
At Kompresory-vzduchotechnika.cz we offer certified safety valves for compressors in various pressure ranges and flow capacities, suitable for air as well as technical gases. Every valve in our offer meets the requirements of the valid standards and is intended for industrial and professional applications. The offer also includes complete compressors and accessories for building safe compressor stations. In the case of specific requirements for pressure, medium or certification we provide technical consultation. The choice of the right valve for your system is a question of safety, not only of technical specification.
Frequently asked questions
What is the difference between the opening and the closing pressure of a safety valve?
The opening pressure is the value at which the valve begins to release the medium. The closing pressure is 0.8 times the opening one, that is approximately 20 % lower, and defines when the valve closes again.
How do you choose a suitable capacity of a safety valve for a specific piece of equipment?
The capacity must reflect the maximum flow generated by the source and must not allow the working pressure to be exceeded by more than 10 to 15 % according to the API 520 or ASME standards.
What to do when the safety valve seeps or does not seal?
Check whether the supply pressure does not exceed the closing pressure of the valve. If it does, insert a reducing valve or lower the setting of the pressure switch. Replace a valve with a damaged seat.
Are safety valves subject to legislative certification?
Yes, industrial safety valves must be certified according to ČSN EN 1488 and the PED 2014/68/EU standards for legal operation in pressure equipment.
Recommended
- Safety valves for reliable release of the overpressure of the medium
- The function of the air receiver: how to increase the efficiency of pneumatic systems - Kompresory-Vzduchotechnika.cz
- The function of the air hose: a 10% increase in the performance of tools - Kompresory-Vzduchotechnika.cz
- How to repair an air leak in a compressor: a guide 2026 - Kompresory-Vzduchotechnika.cz