
In brief:
- The correct choice of compressor oil depends on the type of equipment, operating conditions and the chemical composition of the lubricant. Synthetic oils offer longer change intervals and lower energy consumption compared to mineral oil.
Compressor oil performs four basic functions: it lubricates moving parts, dissipates heat, seals clearances and captures contaminants. An incorrect choice of lubricant shortens bearing life, increases energy consumption, and in extreme cases causes seizure of the rotors or pistons. The choice of oil for an air compressor is governed by three key parameters: the type of base oil, the ISO VG viscosity grade, and the operating conditions of the specific equipment. This guide explains how to correctly select compressor oil, covering everything from chemical composition to change intervals and sample analysis.
What are the main types of compressor oils?
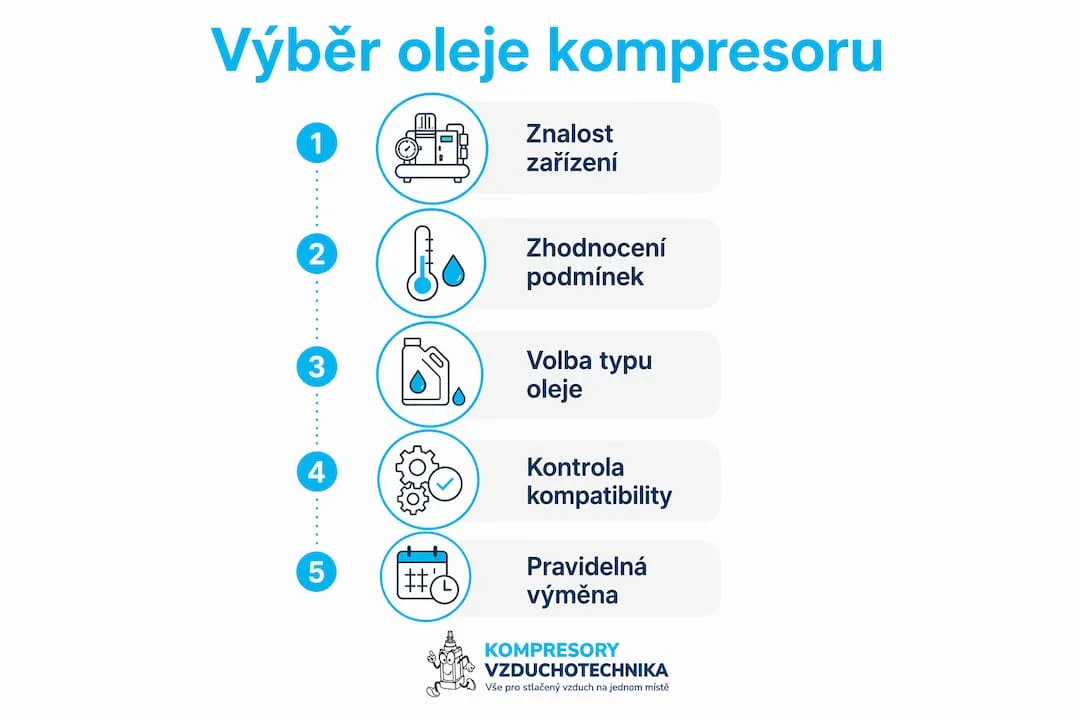
Compressor lubricating oils are divided into four basic categories according to the chemical composition of the base oil. Each category has different properties, different change intervals and different operating costs.
Mineral oil is the most widespread and cheapest option. It is produced by refining crude oil and contains natural impurities that accelerate oxidation at higher temperatures. The change interval for mineral oil ranges from 1,000 to 2,000 operating hours. This means a significantly higher frequency of service interventions compared to synthetic alternatives.
Synthetic PAO-based oil (polyalphaolefin) offers significantly better thermal stability and oxidation resistance. Change intervals reach 4,000–12,000 hours, and synthetic oils reduce the compressor's frictional resistance by 5–8%. Lower friction directly translates into reduced electricity consumption.
Synthetic POE-based oil (polyolester) is used mainly in refrigeration compressors and equipment operating with refrigerants. POE oils have excellent lubricating properties at low temperatures and are compatible with most elastomers. Their disadvantage is higher hygroscopicity, i.e. a tendency to absorb atmospheric moisture.
POE oil is the most common choice for air conditioning compressors with R134a or R1234yf refrigerant. It is always determined by the air conditioning manufacturer's specification — it must not be substituted with PAG oil, which is used in other types of air conditioning compressors, because mixing PAG and POE together creates sludge.
Ester oils combine the properties of PAO and POE. They are used in demanding industrial applications with extreme temperature fluctuations. They are more biodegradable than other synthetic base oils, which is an advantage in environmentally sensitive operations.
| Oil type | Change interval | Friction resistance | Typical use |
|---|---|---|---|
| Mineral | 1,000–2,000 h | Higher | Light industry, DIY |
| Synthetic PAO | 4,000–8,000 h | Lower by 5–8% | Screw compressors |
| Synthetic POE | 4,000–12,000 h | Low | Refrigeration compressors |
| Ester-based | 6,000–12,000 h | Very low | Heavy-duty industry |
In addition to the chemical base, oils for piston compressors must also comply with the DIN 51506 VDL specification. Ash-free oils of the VDL class (for example Paramo Mogul Komprimo VDL 100) reduce the formation of carbon deposits on the valves, extend service intervals and reduce the risk of having to clean the compressor head. For operations with high daily load, this is an economically advantageous solution.
Ventilek advises
For a standard workshop or hobby piston compressor, choose an ash-free VDL class oil with ISO VG 46 viscosity — it's the most commonly specified combination. For a screw compressor, prefer a synthetic PAO oil ISO VG 46 or 68 according to the machine's manual.
Key properties to compare when selecting an oil:
- ISO VG viscosity class (most commonly ISO VG 46 or ISO VG 68 for screw compressors)
- Flash point (at least 200 °C for safe operation)
- Viscosity index (the higher, the more stable the viscosity is under temperature changes)
- Content of antioxidant and anti-corrosion additives
- Compatibility with seals and elastomers in the specific compressor
Reference overview of viscosity classes for piston compressors:
| ISO VG viscosity | Typical use | Note |
|---|---|---|
| ISO VG 32 | Light piston compressors, low temperatures | Suitable for cold environments |
| ISO VG 46 | Standard piston compressors, hobby and workshop use | Most commonly recommended class |
| ISO VG 68 | More powerful piston and two-stage compressors | Higher operating temperatures |
| ISO VG 100 | Heavy-duty industrial compressors, high load | As specified by the manufacturer |
Professional tip: Before switching from mineral to synthetic PAO oil, check the filters and oil channels. Synthetic oils have a higher detergent effect and release old deposits, which can clog filters during the first 200–500 hours of operation.
Cheap mineral oils carry hidden costs in the form of more frequent changes and lower energy efficiency. When calculating total operating costs, you need to include labor costs, equipment downtime, and energy consumption, not just the price of the lubricant itself.
How do operating conditions affect oil selection?
Compressor outlet temperature, intake air quality, and humidity are three factors that determine the suitable oil more than price or brand. Each of them affects the rate of lubricant degradation and the frequency of changes.
The effect of temperature on oil degradation
Temperature is the decisive factor affecting oil oxidation and its lubricating properties. As a general rule, every 10 °C above the recommended operating temperature doubles the rate of lubricant oxidation. Compressors operating at an outlet temperature above 90 °C require synthetic oil with a high viscosity index and strong antioxidant additives.
Modern compressors also have a safety feature: when the lubricating oil temperature reaches 93 °C, the machine automatically shuts down to prevent damage. Repeatedly reaching this threshold is not a sign that the machine is fine, but a symptom of a problem. The most common causes are a fouled oil cooler, a clogged air filter, or excessively high temperature in the compressor room.
Air quality and dustiness of the environment
A dusty environment accelerates oil contamination by solid particles. Abrasive impurities cause wear on bearings and piston rings. Under such conditions, oil change intervals need to be shortened and the frequency of air filter inspections increased.
Air quality factors affecting lubricant selection:
- Concentration of dust and solid particles in the intake air
- Presence of chemical vapors or aggressive gases
- Intake air temperature (higher temperature means lower air density and higher thermal load)
- Operating altitude (affects cooling efficiency)
Humidity and oil oxidation
High humidity in the intake air causes oil emulsification. Water in the oil reduces its lubricating ability and accelerates corrosion of metal surfaces. POE oils are more sensitive to moisture than PAO, so PAO or mineral oils with good hydrophobic properties are recommended for operations with high humidity. Emulsified, milky white oil indicates water contamination and requires immediate replacement regardless of operating hours.
Professional tip: If the compressor operates in an environment with temperatures below 5 °C, choose an oil with a lower ISO VG grade or a special winter formulation. Oil that is too thick during a cold start causes cavitation of the oil pump and insufficient lubrication of bearings in the first seconds of operation.
Adapting viscosity to operating conditions is a direct way of preventing premature wear. ISO VG viscosity is the most important parameter when selecting oil. Viscosity that is too low leads to bearing failure, while viscosity that is too high causes starting problems and increases energy consumption.
Procedure for correctly selecting and changing the oil in a compressor
Proper oil change requires preparation, adherence to the procedure, and compatibility checks. Improvisation at this step causes more failures than neglecting the oil change itself.
Step by step: oil change
- Warm up the compressor to operating temperature. Warm oil is thinner and drains better. Cold oil leaves up to 15% of the old lubricant in the tank.
- Shut down the compressor and release the pressure. Never open the oil tank under pressure.
- Drain the old oil through the drain valve. Let it drain for at least 10 minutes.
- Check the condition of the old oil. Dark color, cloudiness, or foam indicate contamination or oxidation.
- Replace the oil filter. Using an old filter with new oil negates the benefit of the change. A clogged filter restricts oil flow and increases the risk of insufficient lubrication during cold starts.
- Fill the new oil up to the mark on the dipstick. Overfilling causes foaming and oil leakage into the compressed air.
- Run the compressor for 5 minutes and check for leaks. Check the oil level after the first warm-up.
Oil compatibility and the risk of mixing
Mixing incompatible oils, for example PAG with POE, can create gel or sludge. This sludge quickly destroys the compressor bearings. Do not mix synthetic and mineral oils in one system either — their additive packages may react, form sludge, and clog oil channels. When switching from one type to another, thoroughly flush the system with clean oil according to the manufacturer's procedure. Also be careful when mixing oils of different brands with the same viscosity: the resulting properties will approach those of the weaker of the two oils, which can mean failure in demanding operation.
The most common mistakes when changing oil:
- Skipping the oil filter replacement when changing the lubricant
- Topping up a different type of oil into the remainder of the old one (mixing base oils)
- Overfilling the oil tank above the maximum mark
- Using oil with an incorrect ISO VG grade
Analyzing an oil sample every 2,000 hours of operation is an effective way to prevent bearing failure and compressor seizure. Laboratory analysis detects metal particle content, water, oxidation products, and contaminants before they cause a breakdown. This method is referred to as predictive maintenance based on oil condition.
Professional tip: When selecting an industrial compressor, always verify which type of oil the manufacturer specifies. Using a different lubricant may void the warranty, even if the oil is technically comparable.
What are the most common mistakes when choosing compressor oil?
Incorrect lubricant selection is one of the most common causes of premature compressor wear. Most mistakes stem from cost-cutting or lack of information.
The most common errors in practice:
- Using automotive engine oil. Engine oil contains additives intended for combustion engines, not for compressors. Automotive oil causes carbon deposits and rotor seizure after 500–800 hours of operation. This mistake is very widespread in practice, especially among users of piston compressors.
- Mixing different types of oils. Adding a different lubricant to the remaining old oil without verifying compatibility is a direct path to gel or sludge formation in the oil circuit.
- Failing to follow replacement intervals. Extending the replacement interval of mineral oil beyond 2,000 hours leads to oxidation of the lubricant and the formation of varnish on internal surfaces.
- Selecting oil based on price alone. The cheapest oil on the market may not meet the compressor manufacturer's requirements for viscosity or additive content.
"The right compressor oil is neither the cheapest nor the most expensive. It is the one that meets the equipment manufacturer's specifications, suits the operating conditions, and whose replacement intervals are actually followed. Every saving on lubricant comes back as a repair cost."
Selecting the oil for an air compressor according to the equipment manufacturer's recommendation is a basic condition for maintaining the warranty and reliable operation. Following the recommendations of both the oil manufacturer and the compressor manufacturer ensures long-term reliability and predictable operating costs.
How to monitor oil condition and when to plan a replacement?
Monitoring oil condition is the most effective way to prevent unplanned downtime. Regular checking of oil level and condition, including filter cleaning, has been proven to extend compressor service life. Before each start-up, check the oil level using the dipstick or sight glass and inspect oil seals and hoses for visible leaks. Every 250–500 operating hours, replace the oil filter and perform a visual assessment of oil quality.
Laboratory analysis of an oil sample monitors the following parameters:
| Parameter | What it indicates | Limit value |
|---|---|---|
| Water content | Condensation, cooler leak | Above 0.1% |
| Viscosity at 40 °C | Oil degradation or dilution | Deviation above 10% from the new value |
| Fe, Cu, Al content | Bearing and piston wear | According to the manufacturer's standard |
| Total acid number (TAN) | Oxidation and acid formation | Above 2.0 mg KOH/g |
| Solid particle content | Environmental contamination | ISO 4406 class |
Regular oil analysis makes it possible to detect metal fatigue or coolant ingress before a failure occurs. The analysis results serve as a basis for deciding whether to extend or shorten the oil change interval. Besides laboratory analysis, the most reliable diagnostic tool at hand is hearing: a properly lubricated and adjusted compressor runs quietly and evenly, and any change in the sound profile deserves immediate attention. We recommend keeping an oil change log recording operating hours, the lubricant used, and the condition of the oil at the time of change — this will save more time than any other tool during later diagnostics.
Extending oil change intervals significantly reduces operating costs and minimizes downtime, provided the correct type of synthetic oil is used. Switching from mineral to synthetic PAO oil combined with regular sample analysis can reduce the number of oil changes per year by more than half. This has a direct impact on labor, lubricant, and equipment downtime costs. Choosing the right lubricant and saving energy with a compressor go hand in hand — a screw compressor with degraded oil consumes several percent more electrical energy for the same output than the same machine with fresh lubricant.
Key takeaways
Selecting the correct compressor oil requires knowledge of the equipment type, operating conditions, and the chemical composition of the lubricant, with synthetic oils based on PAO or POE offering significantly lower total operating costs than mineral alternatives.
| Point | Details |
|---|---|
| Oil type determines change intervals | Synthetic PAO lasts 4,000–12,000 h, mineral oil only 1,000–2,000 h. |
| ISO VG viscosity is a key parameter | ISO VG 46 is the most common grade for standard reciprocating compressors; using the wrong grade causes bearing failure or starting problems. |
| Automotive oil has no place in a compressor | It causes carbon deposits and rotor seizure after 500–800 hours. |
| Mixing oils is prohibited | PAG with POE forms a gel that destroys bearings within a few hours of operation. |
| A temperature of 93°C is the critical limit | Modern compressors automatically shut down at this temperature; repeated shutdowns indicate a problem in the lubrication or cooling system. |
| Sample analysis every 2,000 hours prevents failures | Laboratory analysis reveals metal wear and contamination before a failure occurs. |
Practical experience: what I've learned about choosing oil
Over years of working with various types of compressors, I've reached one conclusion that holds true without exception. The greatest damage is caused not by the wrong oil, but by the correct oil used at the wrong time or mixed with a different type of lubricant.
In practice, I've seen damaged machines where the last oil change took place three years ago, even though the machine had logged thousands of hours in the meantime. The argument was always the same: the oil level was within normal range. Overheating of the lubricating oil is one of the most recurring causes of unplanned repairs. The automatic shutdown at 93°C is a protection that works, but repeatedly reaching that limit means the system is operating at the edge of its capabilities. I always look for the cause: a clogged oil cooler, a blocked air filter, or too high an ambient temperature in the machine room.
I never rely on the assumption that "the same viscosity will do". Compressor manufacturers test their machines with specific oils and certifications. A replacement oil of a different brand with the same viscosity may not have the same antioxidant or anticorrosive additives. In demanding operation, where the compressor runs 20 hours a day, this difference becomes apparent within a few months.
My recommendation for operators of screw compressors is clear: invest in synthetic PAO oil and set up regular sample collection. The initial costs are higher, but the overall operating costs are lower and downtime is predictable. For piston compressors in light industry or workshops, a quality mineral oil with strict adherence to the change interval is a sufficient choice.
One practical detail rarely mentioned in manuals: when switching from mineral to synthetic oil, perform the first synthetic oil change after 500 hours, not after the standard interval. Synthetic oil releases old deposits, and the first fill will become contaminated faster than the standard interval would suggest.
— Zdeněk
Oils and lubricants for compressors at Kompresory-vzduchotechnika.cz
Choosing the right lubricant is easier with expert support. Kompresory-vzduchotechnika.cz offers technical advice for selecting oil based on the type of compressor, operating conditions and required change intervals.
View oils and lubricants for compressors
The range includes lubricants for piston and screw compressors, mineral and synthetic oils of ISO VG 46 and ISO VG 68 classes, and accessories for oil changes and analysis. The expert team at Kompresory-vzduchotechnika provides consultations for industrial operations as well as individual users. The entire pneumatics and hydraulics range is available online with the option of technical consultation before ordering.
Frequently asked questions
What oil should be used in a screw compressor?
For screw compressors, a PAO-based synthetic oil of ISO VG 46 or ISO VG 68 class is recommended according to the manufacturer's specification. Synthetic oils offer change intervals of 4,000–12,000 hours and reduce frictional resistance by 5–8%.
Can engine oil be used instead of compressor oil?
Engine oil does not belong in a compressor. It contains additives for combustion engines that cause carbon deposits and rotor seizure after 500–800 hours of operation.
How do I know it's time to change the oil in my compressor?
The oil should be changed when the manufacturer's recommended interval is reached, when the lubricant becomes cloudy or darkens, when it foams, or when an increased content of metal particles is found in a sample analysis. Milky white (emulsified) oil indicates water contamination and requires immediate replacement.
Can different types of compressor oils be mixed?
Mixing different types of oils is prohibited. Combining PAG and POE oils forms a gel that destroys the compressor bearings within a few hours of operation. Do not mix synthetic with mineral oil either.
How often should oil analysis be performed on a compressor?
Analysis of an oil sample every 2,000 operating hours is the standard frequency for industrial compressors. Laboratory analysis reveals contamination, oxidation, and metal wear before a failure occurs.
How much oil does a compressor consume and how often does it need topping up?
The fill quantity varies depending on the size of the machine and is always specified in the manufacturer's manual — follow the mark on the dipstick or the oil sight glass. The oil is usually not topped up, but fully replaced at the given interval; if the level keeps dropping, it indicates a leak or oil escaping into the compressed air, which needs to be fixed.
Recommended
- Factors for selecting an industrial compressor: a 2026 guide - Kompresory-Vzduchotechnika.cz
- Basic requirements for a compressor room: guide 2026 - Kompresory-Vzduchotechnika.cz
- Saving energy with a compressor: an expert guide 2026 - Kompresory-Vzduchotechnika.cz
- A list of safety rules for working with a compressor in automotive 2026 - Kompresory-Vzduchotechnika.cz